Product development becomes far more reliable when engineers can test a real metal component before committing to mass production. CAD models and simulation software are valuable, but they cannot fully reproduce real assembly behavior, heat transfer, vibration, wear, surface interaction, or manufacturing limitations. This is why aluminum prototype manufacturing has become an essential step in modern engineering.
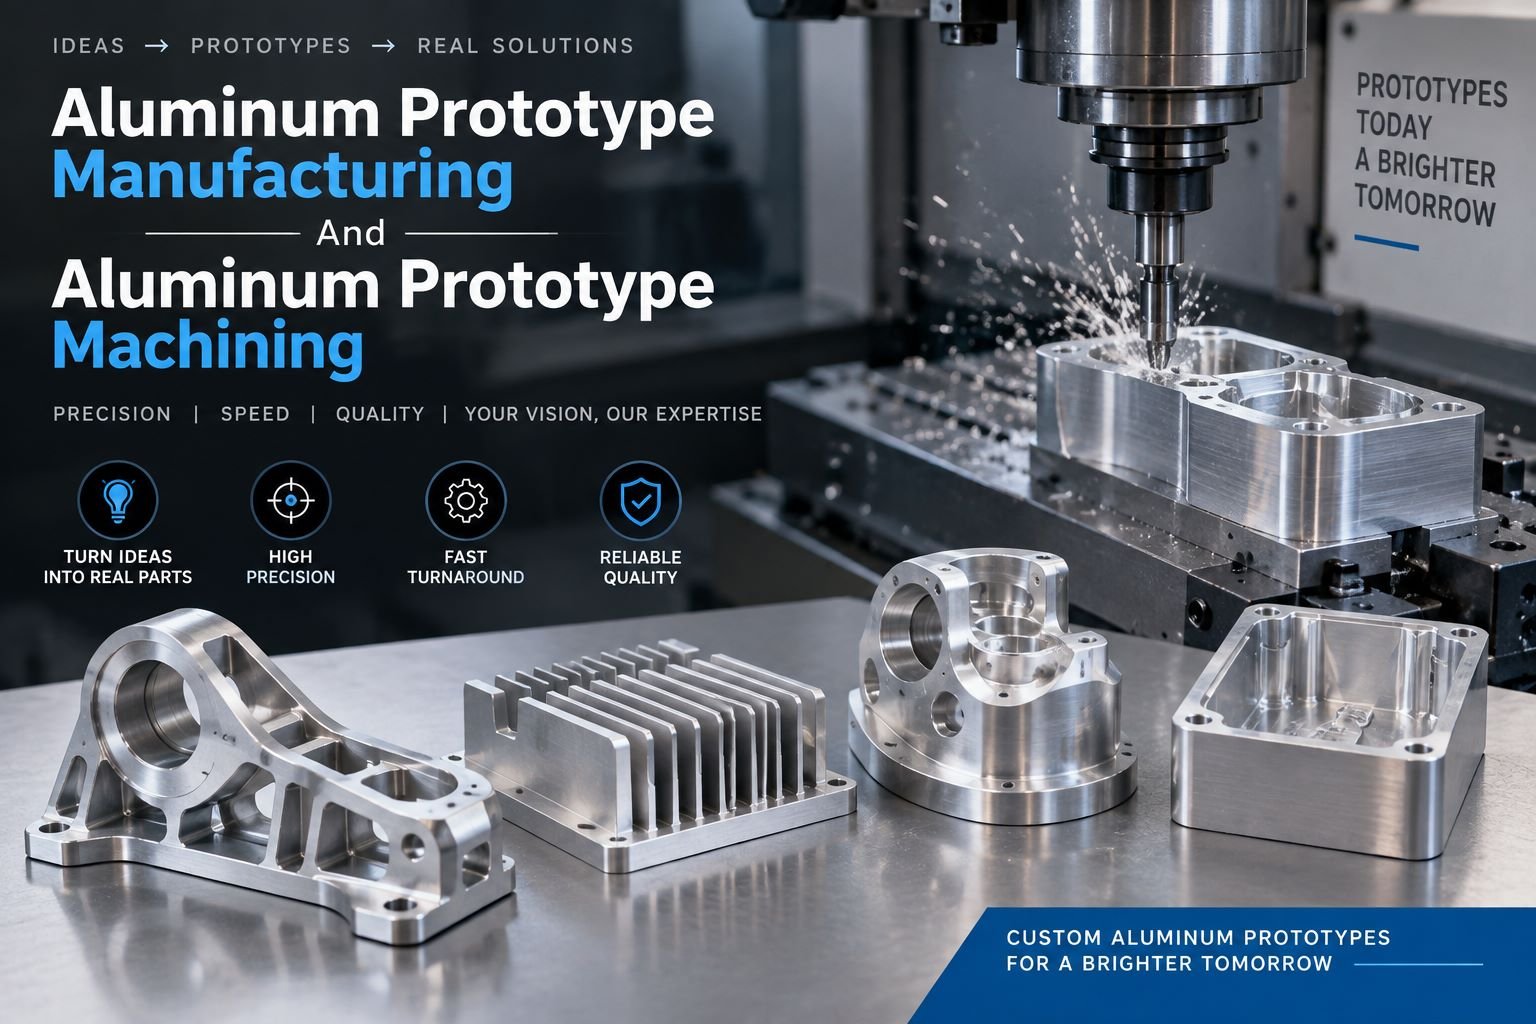
By combining CNC technology, suitable aluminum alloys, precision inspection, and design-for-manufacturing principles, manufacturers can create realistic components for functional testing. At the center of this process is aluminum prototype machining, which transforms raw aluminum stock into accurate, test-ready parts without requiring expensive molds or dedicated production tooling.
Why Aluminum Is a Strategic Prototyping Material
Aluminum is widely selected because it provides a useful balance between strength, weight, machinability, corrosion resistance, and cost. It is significantly stronger and more rigid than many prototyping plastics while remaining easier to machine than numerous steels.
Its thermal conductivity also makes aluminum valuable for products involving heat management.
Typical applications include:
- Electronic housings
- Automotive components
- Aerospace brackets
- Robotics assemblies
- Medical equipment
- Industrial fixtures
- Heat sinks
- Camera housings
- Machine frames
- Consumer electronics
For functional testing, aluminum prototype manufacturing allows engineers to evaluate components under conditions that closely represent actual use.
The Complete Aluminum Prototype Development Process
A successful prototype should follow a controlled engineering workflow rather than simply moving directly from a CAD model to machining.
The process normally includes:
- Product requirement analysis
- CAD model evaluation
- Material selection
- Design-for-manufacturing review
- Tolerance definition
- CNC programming
- Rough machining
- Finish machining
- Secondary operations
- Dimensional inspection
- Surface finishing
- Functional validation
Each stage contributes to final prototype quality.
For example, incorrect tolerance selection can increase cost, while poor material selection may produce inaccurate test results.
Understanding CNC Aluminum Prototype Machining
Aluminum prototype machining removes material from solid aluminum stock using computer-controlled cutting equipment.
CNC machines follow programmed toolpaths created using CAM software. These instructions control tool movement, spindle speed, feed rate, depth of cut, and machining sequence.
Common processes include:
- CNC milling
- CNC turning
- Drilling
- Boring
- Reaming
- Threading
- Tapping
- Engraving
Milling is typically used for blocks, housings, plates, pockets, and complex surfaces, while turning is more appropriate for cylindrical parts such as shafts, spacers, bushings, and threaded components.
Three-Axis Versus Five-Axis CNC Machining
Choosing the right machining configuration depends largely on part geometry.
| Feature | 3-Axis CNC | 5-Axis CNC |
| Machine movement | X, Y, Z | X, Y, Z plus rotation |
| Part complexity | Simple to moderate | Complex |
| Setup requirements | Usually higher | Often lower |
| Tool accessibility | Limited | Excellent |
| Typical cost | Lower | Higher |
| Best application | Standard components | Precision complex parts |
Five-axis aluminum prototype machining can machine several surfaces without repeatedly repositioning the component.
Reducing setups can improve feature alignment and dimensional consistency.
Selecting the Correct Aluminum Alloy
Different aluminum alloys provide different mechanical properties.
| Alloy | Main Characteristics | Suitable Applications |
| 6061 | Balanced strength, excellent machinability | General engineering |
| 7075 | Very high strength | Aerospace, performance parts |
| 2024 | Strong fatigue resistance | Aircraft components |
| 5052 | Excellent corrosion resistance | Sheet metal assemblies |
| 6082 | Good structural properties | Machinery and frames |
6061 is particularly popular for aluminum prototype manufacturing because it offers good strength, dimensional stability, machinability, and finishing capability.
7075 is generally selected when significantly greater mechanical strength is required.
Material selection should always reflect the intended operating environment.
Designing Aluminum Parts for Better Machining
Good prototype design should consider how cutting tools physically access each feature.
Several design decisions can have a major impact on manufacturing efficiency.
Internal corners should include reasonable radii because milling cutters cannot create perfectly sharp internal corners.
Deep narrow pockets should also be minimized because long cutting tools may experience vibration and deflection.
Very thin walls can deform during machining, making dimensional accuracy difficult to maintain.
Designers should also avoid specifying extremely tight tolerances unless those tolerances directly affect product function.
Understanding Machining Tolerances
Tolerance defines the acceptable variation from a specified dimension.
Critical features may include:
- Bearing locations
- Press-fit holes
- Sealing surfaces
- Precision bores
- Alignment features
- Mechanical interfaces
Tighter tolerances generally require slower machining, additional tool changes, controlled environments, and more inspection.
Therefore, applying precision requirements only where necessary can make aluminum prototype machining more economical.
Surface Finish and Post-Machining Treatments
Prototype finishing can serve both functional and cosmetic purposes.
Common treatments include:
- Anodizing
- Hard anodizing
- Bead blasting
- Polishing
- Brushing
- Painting
- Powder coating
- Chemical conversion coating
Anodizing is one of the most common options because it creates a protective oxide layer that improves corrosion resistance and appearance.
Bead blasting produces a uniform matte texture and can remove minor visible machining marks.
Surface finishing should be considered during design because certain treatments can slightly alter dimensions.
Quality Inspection for Precision Aluminum Prototypes
Quality control confirms whether a machined component matches its engineering drawing and CAD model.
Inspection may involve:
- Calipers
- Micrometers
- Bore gauges
- Thread gauges
- Height gauges
- Pin gauges
- Optical measurement systems
- Coordinate measuring machines
For complex prototypes, a coordinate measuring machine can inspect multiple geometric features with high accuracy.
Reliable aluminum prototype manufacturing should also include material verification, visual inspection, documentation, and dimensional reporting when required.
Factors That Determine Prototype Cost
Prototype pricing is influenced by machining difficulty rather than simply part size.
Important cost factors include:
| Factor | Cost Impact |
| Complex geometry | Longer programming and machining |
| Tight tolerances | Greater precision requirements |
| Deep cavities | Longer tools and slower cutting |
| Multiple setups | Additional labor |
| Small quantity | Higher cost per component |
| Specialty alloy | Higher material expense |
| Finishing | Additional processing |
Design simplification can reduce cost considerably without affecting functionality.
Standard holes, realistic tolerances, generous internal radii, and common aluminum grades are particularly helpful.
Frequently Asked Questions
1. What is aluminum prototype manufacturing?
It is the production of low-volume aluminum components for engineering testing, design validation, and product development.
2. Why choose aluminum for prototypes?
Aluminum combines low weight, good strength, machinability, corrosion resistance, and thermal conductivity.
3. What is aluminum prototype machining?
It is the CNC-based removal of material from aluminum stock to produce accurate prototype components.
4. Is aluminum 6061 suitable for prototyping?
Yes. It is one of the most widely used aluminum alloys for general-purpose machined prototypes.
5. When should 7075 aluminum be selected?
7075 is suitable when higher mechanical strength is required.
6. Can aluminum prototypes have threaded features?
Yes. CNC machining can produce internal and external threads.
7. Why are tight tolerances more expensive?
They require additional machine control, inspection, tooling, and production time.
8. Can complex prototypes be manufactured?
Yes. Multi-axis CNC machining can create highly complex geometries.
9. Can prototype parts receive production-quality finishes?
Yes. Anodizing, polishing, powder coating, painting, and other finishes can be applied.
10. What files should be supplied to a manufacturer?
Provide 3D CAD files, engineering drawings, material requirements, tolerances, quantities, and finishing specifications.