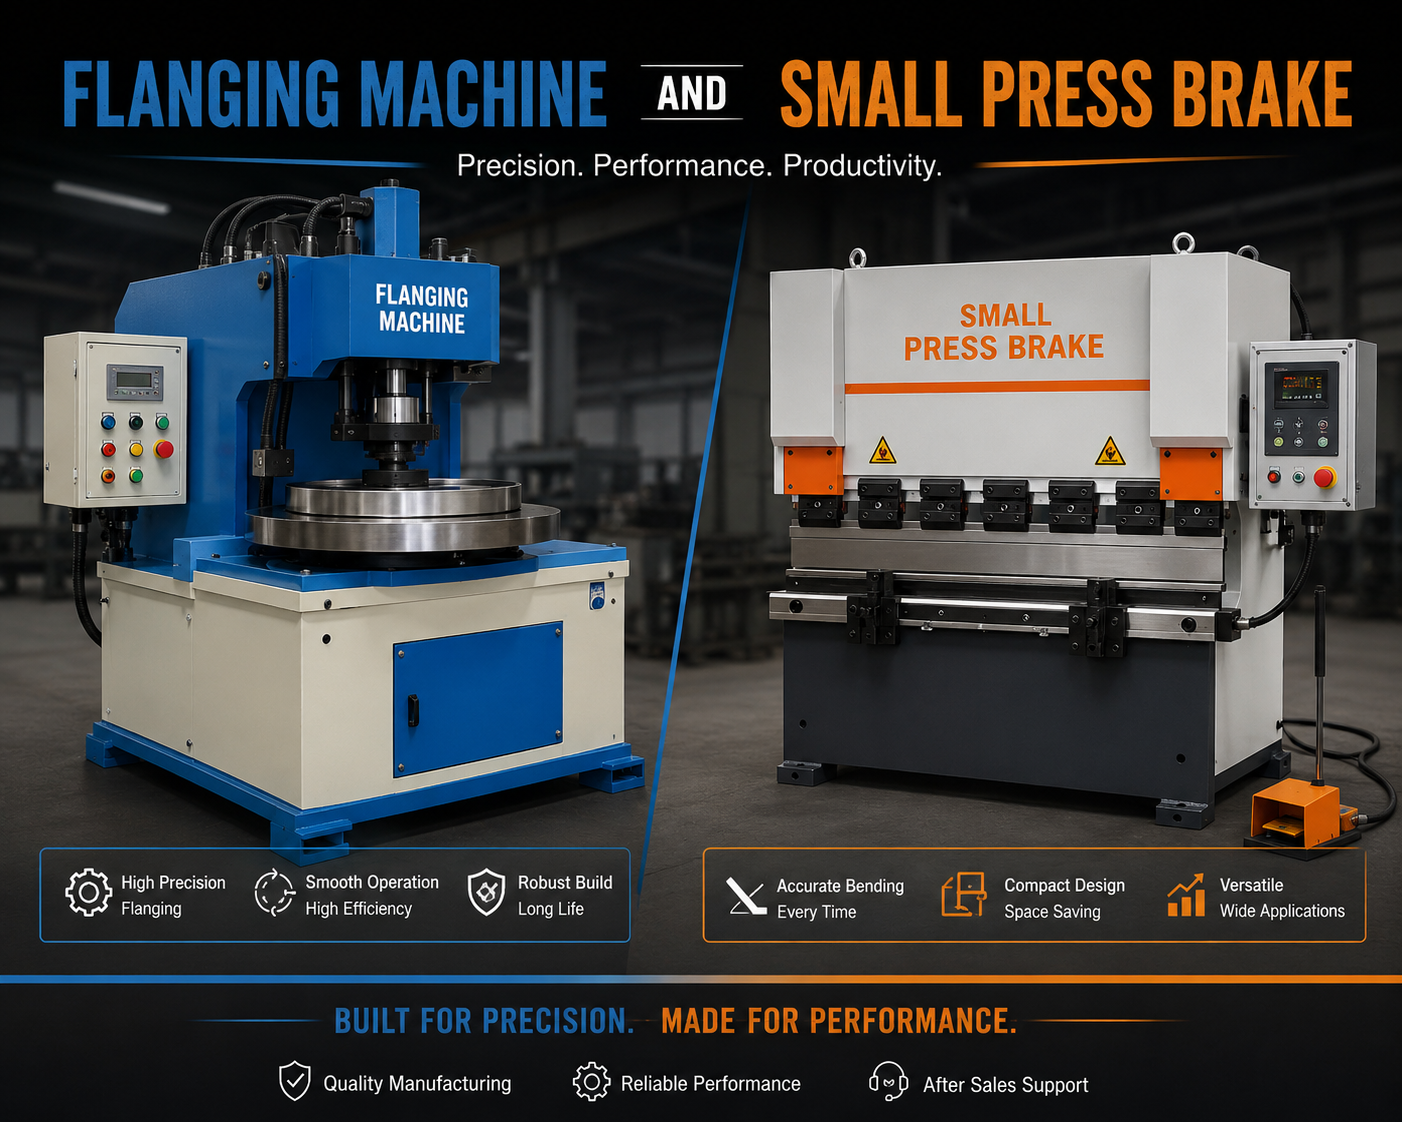
Modern manufacturers need accuracy, repeatability, faster setup, reduced waste, and flexibility for different jobs. This is where equipment such as a flanging machine and a small press brake becomes important.
Both machines support metal forming, but they perform very different jobs. A flanging machine specializes in creating formed edges around sheet metal components, while a small press brake produces straight bends, folds, channels, and other profiles.
Understanding how each machine fits into the production process can help workshops select equipment that improves productivity rather than simply adding another machine to the factory floor.
Why Choosing the Correct Forming Machine Matters
Using the wrong equipment for a forming operation can increase production time and create unnecessary quality problems.
Manufacturers generally expect modern machines to provide:
- Consistent dimensions
- Reduced manual correction
- Faster production cycles
- Lower scrap rates
- Cleaner finished components
- Better repeatability
- Easier operator control
The correct machine can also simplify later operations such as welding, assembly, fastening, and finishing.
Flanging Machine: More Than Simple Edge Bending
A flanging machine is designed to reshape the edge of a sheet metal component. The resulting flange can provide mechanical strength, create a joining area, or prepare the component for further manufacturing.
Flanging is especially useful when producing circular, curved, or cylindrical components.
For example, a metal tank may require a formed edge around its top section so that another component can be welded or attached securely. Creating this edge manually can lead to uneven results, while dedicated flanging equipment provides better consistency.
How Flanging Changes the Strength of a Component
A flat metal edge can flex relatively easily. Once the edge is formed into a flange, its geometry changes, which can improve rigidity.
Flanges are often created to:
- Reinforce thin metal sections
- Improve edge stability
- Support welding
- Create bolted joints
- Provide sealing surfaces
- Help components align during assembly
Because of these functions, a flanging machine contributes not only to shape but also to overall product performance.
Understanding Different Flanging Requirements
Every flange does not have the same dimensions.
Manufacturers may require:
External Flanging
The metal edge is formed outward from the main component.
Internal Flanging
The edge is turned toward the inside of the workpiece.
Circular Edge Forming
This process is commonly used on discs, vessel heads, drums, and round covers.
Controlled Forming
Gradual forming can help prevent excessive stretching, wrinkling, or cracking, particularly when working with difficult materials or complex geometries.
Where Flanging Machines Deliver the Most Value
A flanging machine is commonly associated with industries producing curved or round sheet metal products.
Typical applications include:
- Industrial storage tanks
- HVAC duct systems
- Metal drums
- Pressure vessel components
- Exhaust parts
- Circular lids
- Ventilation fittings
- Food-processing vessels
- Metal containers
- General fabricated assemblies
The required machine design depends heavily on material thickness, component diameter, flange size, and production quantity.
Why Small Press Brakes Are Useful for Flexible Manufacturing
A small press brake is designed for workshops that need accurate bending but may not require a full-size high-tonnage machine.
It bends material by pressing sheet metal between an upper punch and lower die.
Different tooling configurations allow operators to produce multiple profiles without purchasing a completely separate machine for every job.
This makes a small press brake attractive for custom fabrication, maintenance workshops, prototype development, and short-to-medium production runs.
Typical Jobs for a Small Press Brake
Compact press brakes can manufacture a surprisingly wide range of products.
Common applications include:
- Metal brackets
- Electrical enclosure parts
- Equipment covers
- Small trays
- Channels
- Control panels
- Metal shelves
- Machine guards
- Cabinet components
- Automotive support parts
The same machine may produce several different component types during one working day.
What Makes a Small Press Brake Different from Large Equipment?
Machine size is not the only difference.
A compact press brake is generally designed around smaller components and shorter bending lengths.
Potential advantages include:
- Smaller factory footprint
- Easier installation
- More convenient handling of small parts
- Faster job changes
- Lower space requirements
- Good suitability for custom work
However, available tonnage and bending length must still match the material being processed.
Flanging Machine vs Small Press Brake
| Requirement | Flanging Machine | Small Press Brake |
| Main process | Edge forming | Straight-line bending |
| Best suited for | Round and curved components | Panels and fabricated sections |
| Common tooling | Rollers and forming tools | Punch and die |
| Bracket production | Limited | Excellent |
| Tank edge forming | Excellent | Application dependent |
| Multi-angle work | Limited | Highly flexible |
| Prototype production | Moderate | Excellent |
| Specialized production | Excellent | Broad application |
The machines are therefore often complementary rather than interchangeable.
What Determines Press Brake Bending Quality?
Several variables influence the result produced by a small press brake.
Material Thickness
Thicker sheet requires more bending force.
Material Strength
Stainless steel may require more force than mild steel of a similar thickness.
Die Opening
The die opening affects required tonnage and bend radius.
Bend Length
A longer bend generally requires more total force than a short bend made from the same material.
Ignoring these factors can result in incorrect angles, machine overload, or poor component quality.
Why the Backgauge Is Important
A press brake backgauge helps position the workpiece before bending.
For example, if a component requires a 30 mm flange, the backgauge helps locate the sheet so that the bend is produced at the correct distance from its edge.
Accurate positioning is especially important when producing hundreds of identical parts.
Modern systems may use digital or CNC-controlled backgauges to improve repeatability.
Important Factors When Buying a Flanging Machine
Before purchasing a flanging machine, manufacturers should identify the largest and smallest components they expect to produce.
Important considerations include:
- Maximum sheet thickness
- Material grade
- Minimum diameter
- Maximum diameter
- Required flange width
- Desired forming radius
- Production volume
- Tooling availability
- Adjustment time
- Automation level
Machine selection based only on price may result in limited production capability later.
How to Select a Small Press Brake
Choosing a small press brake requires a similar production-based approach.
Manufacturers should evaluate:
- Available tonnage
- Maximum bending length
- Stroke
- Daylight opening
- Backgauge accuracy
- Tool compatibility
- CNC or manual control
- Machine frame rigidity
- Safety systems
Some additional capacity can be useful when future product requirements are likely to increase.
Preventing Common Forming Problems
Good machine selection alone cannot eliminate production errors.
Common problems include:
Inconsistent Bend Angles
Possible causes include worn tooling, varying sheet thickness, machine deflection, or incorrect setup.
Cracked Edges
Cracking may occur when a flange or bend radius is too tight for the selected material.
Surface Marks
Dirty or damaged tools can leave visible impressions on finished components.
Dimensional Variation
Incorrect positioning or backgauge settings can produce inconsistent component dimensions.
Regular inspection helps identify these problems before large batches are completed.
How Manufacturers Can Improve Daily Productivity
Production efficiency can often be improved through simple working practices.
Consider:
- Grouping similar jobs together
- Storing proven machine settings
- Preparing tooling before production
- Inspecting the first finished component
- Monitoring tool wear
- Keeping machines clean
- Training operators properly
- Following scheduled maintenance
These practices reduce unnecessary setup and improve repeatability.
Frequently Asked Questions
1. What is a flanging machine?
A flanging machine is equipment used to form controlled edges or rims on sheet metal components.
2. Why are flanges created?
Flanges may strengthen components, provide joining surfaces, support sealing, or simplify assembly.
3. Can flanging machines process circular parts?
Yes. Circular component forming is one of the major applications of many flanging machines.
4. What does a small press brake manufacture?
A small press brake can manufacture brackets, boxes, channels, panels, covers, and many other bent metal parts.
5. Is a small press brake suitable for low-volume work?
Yes. Compact press brakes are particularly useful for prototypes and smaller production batches.
6. What determines required press brake force?
Material thickness, tensile strength, bending length, tooling, and die opening influence force requirements.
7. Can stainless steel be flanged?
Yes, provided the machine has sufficient capacity and suitable tooling.
8. What causes metal to return after bending?
This phenomenon is called springback and occurs because part of the material’s elastic deformation recovers after pressure is removed.
9. Why is tooling important?
Correct tooling helps control bend angle, radius, flange geometry, and finished surface quality.
10. Can one press brake produce different products?
Yes. Changing tooling and machine settings allows a press brake to handle many component designs.